Choosing the right Ultra-Fine Cotton Swab supplier requires more than comparing prices. Global buyers need dependable quality, consistent production, and clear communication across borders. A reliable supplier should explain cotton fiber origin, tip dimensions, shaft materials, packaging methods, and inspection procedures. Small details matter. A loose tip can affect laboratory handling, cosmetic application, or precision cleaning.
This guide introduces the 2026 Best Ultra-Fine Cotton Swab Suppliers for Global Buyers. It focuses on manufacturers with practical export experience, documented quality systems, and responsive customer support. Supplier evaluation should include factory audits, product samples, batch records, and certificates of analysis. Buyers should also confirm labeling requirements, packaging language, shipping capacity, and destination-market compliance before placing large orders.
No supplier is perfect.
Even experienced manufacturers may face material delays, inconsistent lots, or communication gaps. That is why a careful purchasing process remains essential. Ask how suppliers control lint, moisture, fiber density, and tip bonding during production. Review whether inspection results are traceable to specific batches. A clean sample is useful, but it does not replace ongoing quality verification.
The suppliers discussed here are assessed through a practical, evidence-based lens. Their manufacturing capabilities, customization options, export readiness, and service reliability all receive attention. Some may offer strong pricing but limited flexibility. Others may provide excellent documentation at a higher cost. This guide helps buyers compare those trade-offs clearly and choose a partner that fits their technical, commercial, and compliance needs.
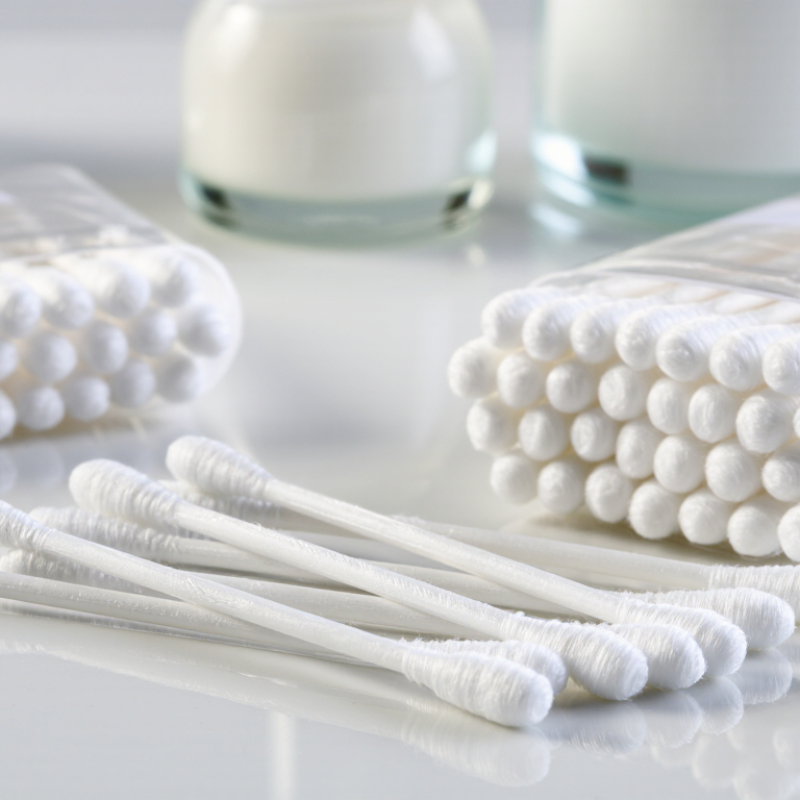
For global buyers, ultra-fine cotton swabs should be evaluated by measurable specifications, not appearance alone. Check tip diameter, cotton weight, fiber uniformity, shaft length, and shedding level. A narrow tip may reach small grooves, while a loose wrap can leave fibers behind. Test it.
Experienced purchasers should request samples from each production lot. Inspect the swab under magnification and record residue after a controlled cleaning test. For laboratory or medical-related applications, confirm applicable quality documents, packaging conditions, and sterilization status when required. Cotton purity, moisture control, and sealed packaging also affect storage stability. No single tip size fits every application.
Common uses include cleaning optical parts, sampling small surfaces, applying liquids, and removing dust from precision equipment. Buyers should define the intended surface before approving a design. Abrasive shafts may damage delicate coatings, even when the cotton tip looks soft. This detail is easy to miss.
Supplier terms should clearly state minimum order quantity, sample policy, production lead time, inspection method, carton dimensions, and delivery terms. Ask for a certificate of analysis and traceability records. A low price can become expensive when lint, inconsistent sizing, or delayed replacement shipments interrupt production. Specifications may look perfect on paper, but actual handling can reveal weaknesses. Recheck assumptions after the first shipment.
For global buyers, ultra-fine cotton swab selection should begin with quality systems, not price. ISO 13485:2016 shows that a supplier controls design, production, traceability, risk management, and corrective actions. From February 2026, U.S. QMSR requirements align more closely with ISO 13485 principles. Still, certification alone proves little about daily performance.
Ask for a current certificate, audit scope, expiration date, and site address. Check whether the certificate covers cotton swabs, packaging, and related production activities. Request batch records, incoming-material checks, bioburden controls, and complaint-handling procedures. A reliable supplier should explain how each lot is identified, inspected, released, and recalled when necessary. During an audit, inspect clean areas, sealed cartons, calibration labels, and employee training records. Small details matter.
Tips: Ask for three recent sample lots. Compare tip diameter, fiber shedding, shaft strength, and packaging seals. Review change-control records before approving a long-term contract. Keep written acceptance criteria. Do not rely on verbal promises.
Practical experience also requires testing samples under actual use conditions. A swab may look precise but bend against a narrow surface. One shipment may perform differently if moisture control changes. That is a weakness worth discussing openly. Suppliers should document root-cause investigations and corrective actions, rather than hide isolated failures. Buyers should also record their own inspection results. Neither side is perfect. A transparent QMS makes problems visible early.
For global buyers of ultra-fine cotton swabs, ISO 2859-1 AQL sampling turns quality control into a repeatable process. A supplier defines each production lot before inspection. The lot may contain 20,000 packed swabs from one shift, material batch, and machine setup. Inspectors then select the inspection level and code letter according to lot size. General Inspection Level II is often a practical starting point, but the buyer should confirm it.
Small details matter.
The sample is checked for tip diameter, cotton alignment, fiber shedding, shaft bonding, cleanliness, and package sealing. Inspectors compare results with agreed AQL limits for critical, major, and minor defects. A loose tip may be major. Visible contamination may be critical. Slight cosmetic variation may be minor. The acceptance and rejection numbers must be recorded before testing begins, not changed after results appear.
Experienced quality teams use random selection from different cartons and pallet positions. They photograph defects and link findings to lot numbers, operators, and equipment settings. This creates evidence beyond a passing inspection report. Sampling is not a guarantee that every swab is perfect. It is a risk-control method. That limitation deserves honest attention. A supplier may also retain samples, review recurring defects, and apply tightened inspection after repeated failures. One weakness remains: rushed sampling can hide process variation. For that reason, trained inspectors, calibrated tools, clean lighting, and independent review are essential for reliable export decisions.
2026 Best Ultra-Fine Cotton Swab Suppliers for Global Buyers
Sterility validation separates dependable cotton swab suppliers from attractive catalog listings. ISO 11135 governs ethylene oxide sterilization, while ISO 11137 covers radiation sterilization. Each method requires documented process development, validation, and routine control.
For ultra-fine cotton swabs, buyers should examine the actual product configuration. Fiber density, wooden or polymer shafts, adhesive points, and packaging can affect sterilization performance. Under ISO 11135, suppliers should provide evidence of bioburden testing, cycle development, load configuration, and residual EO control. Under ISO 11137, dose setting, dose verification, and regular dose audits deserve equal attention. A clean certificate is not enough. Validation must represent the finished, packaged swab. Otherwise, the paperwork may look complete while the real load behaves differently. That is an uncomfortable possibility, but it deserves review.
Tips: Request validation summaries, sterilization batch records, and packaging integrity data. Check whether the tested configuration matches your ordered length, tip size, and pouch format. Ask how deviations are investigated and corrected. Independent laboratory reports can strengthen confidence, although they should not replace supplier process records. Also review storage conditions and expiry claims. Sterility may be validated, yet packaging performance can weaken during transport or extended warehouse storage. Suppliers with practical experience usually explain these limits clearly, rather than promising flawless results.
| Evaluation Dimension | Reference Data or Acceptance Point | ISO 11135: Ethylene Oxide Sterilization | ISO 11137: Radiation Sterilization | Supplier Evidence Required | Global Buyer Check |
|---|---|---|---|---|---|
| Ultra-Fine Cotton Tip | Typical RFQ reference range: approximately 1–3 mm tip diameter. The exact size must be defined by the intended application and drawing. | ISO 11135 does not define cotton-tip dimensions. Confirm that the sterilization cycle does not deform, discolor, or loosen the tip. | ISO 11137 does not define cotton-tip dimensions. Confirm that the selected radiation dose does not cause unacceptable brittleness or color change. | Approved product drawing, dimensional inspection report, tip-integrity test, and retained-sample photographs. | Verify tip diameter, length, density, lint level, and application compatibility before approval. |
| Swab Shaft and Overall Length | Common medical and laboratory procurement ranges are approximately 70–150 mm overall length, subject to the approved design. | Validate packaging and load configuration so that the EO process reaches all product locations. | Validate dose distribution throughout the packed product and confirm that the shaft remains functional after irradiation. | Product specification, material declaration, dimensional report, and packaging-load configuration. | Match shaft length, diameter, rigidity, and break resistance to the intended sampling procedure. |
| Cotton Fiber and Lint Control | Cotton composition, absorbency, extractables, and lint limits should be defined in the product specification; ISO 11135 and ISO 11137 do not establish universal cotton-swab lint limits. | Include bioburden control and product/material compatibility assessment because moisture and residual process conditions can affect cotton performance. | Assess possible radiation-related changes to fiber strength, color, odor, and extractables at the validated dose range. | Fiber composition statement, lint test method, absorbency data, extractables assessment, and change-control records. | Require a defined lint acceptance limit and test method instead of relying only on visual inspection. |
| Sterilization Route | The supplier should declare whether the product is supplied sterile by EO, gamma radiation, or electron-beam radiation. | ISO 11135 specifies requirements for the development, validation, and routine control of an EO sterilization process for medical devices. | ISO 11137 specifies requirements for the development, validation, and routine control of radiation sterilization for health-care products. | Sterilization method statement, validated process scope, sterilization facility qualification, and current certificate status. | Confirm that the declared method matches the import dossier, labeling, and intended market requirements. |
| Bioburden Program | Bioburden must be measured using a documented sampling plan and a validated or verified recovery method appropriate to the product. | Bioburden data support EO process definition, monitoring, and the selection of the sterilization approach. | Bioburden data support radiation dose establishment and ongoing dose-audit activities. | Recent bioburden trend reports, sampling plan, recovery-efficiency data, organism identification procedure, and laboratory qualifications. | Review trends by production line, product configuration, packaging type, and manufacturing site. |
| Sterility Assurance Level | A commonly specified target for terminally sterilized medical devices is an SAL of 10-6; the applicable requirement depends on the product and market. | Demonstrate the validated EO process and routine controls that support the specified SAL. | Demonstrate the validated radiation dose and routine dose-audit program that support the specified SAL. | Validation report, dose or cycle justification, process challenge data, and product-family rationale. | Confirm that the SAL claim applies to the exact cotton-swab configuration and packaging presentation being purchased. |
| EO Residuals | EO residual limits are product- and exposure-dependent and should be evaluated against the applicable medical-device requirements, including ISO 10993-7 where relevant. | Required. Establish aeration conditions and test EO, ethylene chlorohydrin, and ethylene glycol where applicable. | Not applicable to radiation sterilization unless the product has also been exposed to EO. | Residual-gas test reports, aeration-cycle records, laboratory method details, and acceptance criteria. | Request results from the actual product and packaging configuration, not only generic process data. |
| Radiation Dose Range | A commonly used industrial radiation sterilization dose is 25 kGy, but the approved dose must be established and justified for the product. | Not applicable unless EO is the selected sterilization process. | Establish the minimum sterilization dose and maximum acceptable dose, with dose mapping and periodic dose audits. | Dose-establishment report, dose-map results, dosimetry records, routine dose-audit schedule, and material-compatibility assessment. | Confirm whether the stated dose is a validated range or merely a nominal irradiation setting. |
| Packaging Sterile Barrier | Packaging should maintain sterility through specified distribution and shelf-life conditions. Packaging performance is normally evaluated using ISO 11607 requirements where applicable. | Confirm EO permeability, aeration compatibility, seal integrity, and the absence of process-induced package damage. | Confirm radiation compatibility of the pouch, header, sealant, adhesive, and printed materials. | Packaging specification, seal-strength data, visual inspection criteria, integrity testing, and transportation simulation results. | Check pouch dimensions, peel performance, labeling legibility, and packaging quantity per shipping carton. |
| Sterility Validation Approach | Validation should be documented, reproducible, and linked to the defined product family, worst-case configuration, and routine production process. | Include installation and operational qualification, performance qualification, cycle definition, load configuration, and routine monitoring. | Include dose establishment or verification, dose mapping, maximum-dose evaluation, and routine dosimetry controls. | Signed validation protocol and report, deviation assessment, requalification plan, and change-control procedure. | Ensure validation covers the same raw material, tip size, packaging, loading pattern, and manufacturing location. |
| Process Monitoring and Release | Each sterilized batch should have traceable release records linking product lot, sterilization lot, process parameters, and disposition decision. | Monitor critical EO process parameters such as temperature, humidity, gas exposure, pressure, and aeration conditions as defined by the validated cycle. | Monitor delivered dose, product loading, dosimeter results, and irradiation-cycle records according to the validated process. | Certificate of sterilization, batch release record, process chart, deviation log, and traceability statement. | Require lot-level records and a defined procedure for handling out-of-specification or interrupted sterilization cycles. |
| Shelf Life and Storage | Shelf life must be supported by packaging and product stability data under defined temperature and humidity conditions. | Evaluate long-term effects of EO exposure, aeration, packaging aging, and storage conditions. | Evaluate radiation effects on cotton fibers, shaft materials, adhesives, packaging, and printed information over the claimed shelf life. | Accelerated-aging rationale, real-time aging plan or data, storage specification, and packaging integrity results. | Confirm remaining shelf life at shipment and the required storage conditions for each destination market. |
| Quality Management and Regulatory File | Global buyers should assess the supplier’s quality system, document control, complaint handling, CAPA, supplier control, and change notification process. | Sterilization validation records should be controlled within the applicable quality-management system. | Radiation validation and dose-audit records should be controlled within the applicable quality-management system. | Current quality-system certificate, audit summary, technical file index, inspection records, and change-notification policy. | Verify certificate scope, manufacturing-site address, validity dates, and product coverage before commercial approval. |
| Batch Traceability | Traceability should connect raw-material lots, cotton preparation, assembly, packaging, sterilization, inspection, and shipment records. | Include sterilization load number, cycle number, EO batch record, aeration record, and release status. | Include irradiation lot number, dose record, dosimeter identification, and release status. | Sample certificate of analysis, sample certificate of sterilization, lot-code structure, and recall-traceability procedure. | Conduct a mock traceability exercise from finished carton back to raw-material and sterilization records. |
| Recommended RFQ Documentation Package | A complete technical submission should allow comparison without relying on undisclosed brand or company claims. | Request EO validation summary, residual report, bioburden trend, cycle specification, and batch-release example. | Request radiation validation summary, dose-establishment report, dose map, bioburden trend, and batch-release example. | Product drawing, specification sheet, sterilization certificate, packaging validation summary, stability data, and change-control terms. | Compare suppliers using identical documentation requirements, sample quantities, acceptance criteria, and audit conditions. |
Global buyers should assess ultra-fine cotton swab suppliers beyond unit price. EU MDR 2017/745 requires evidence based on intended use, risk classification, labeling, and post-market controls. A cosmetic sampling swab may follow a different pathway from a device used for clinical specimen collection. The distinction matters. MedTech Europe’s 2024 Facts & Figures estimates Europe’s medical technology market at about €170 billion, showing the scale of this regulated purchasing environment.
Supplier costs usually include material, sterilization, packaging, testing, technical files, and conformity assessment. Budget quotations can hide these expenses. For small orders, tooling and validation may raise total costs by 20–40%, based on common procurement benchmarks rather than a universal tariff. Lead times often reach 8–16 weeks for customized, sterile products. Stock items may ship sooner, but documentation can still delay release. The European Commission’s MDR transition guidance also shows why notified-body availability remains a practical concern for manufacturers.
Tips: Request a declaration of conformity, ISO 13485 certificate, biocompatibility evidence, sterility validation, and batch-level traceability. Ask for separate prices for samples, regulatory documents, and recurring production. Confirm whether the quoted lead time includes testing and EU release checks. One overlooked detail is cotton-fiber shedding. It may affect microscopy, swab recovery, or laboratory cleanliness. Suppliers should provide test methods, not vague assurances. A careful comparison is slower, but a cheap quote is sometimes incomplete.
Check tip diameter, cotton weight, fiber uniformity, shaft length, and shedding level. A narrow tip may reach small grooves. Test actual samples, not appearance alone.
Different lots may show changes in sizing, bonding, or fiber shedding. Inspect samples under magnification and record residue after controlled cleaning. Paper specifications can still miss handling problems.
Common uses include optical parts, small surfaces, precision equipment, and liquid application. Define the surface before approval. A hard shaft may scratch a delicate coating.
Inspect tip diameter, cotton alignment, fiber shedding, shaft bonding, cleanliness, and package sealing. Visible contamination may require serious attention. Slight cosmetic variation may be minor.
It creates a repeatable inspection method for defined production lots. Inspectors select samples using the lot size and inspection level. Acceptance numbers must be agreed before testing begins.
No. Sampling controls risk; it does not inspect every unit. Random selection should cover different cartons and pallet positions. Rushed sampling can hide process variation. That weakness matters.
Request validation summaries, sterilization batch records, packaging data, and traceability documents. For gas processing, review bioburden, cycle development, load setup, and residual control. For radiation processing, review dose setting and dose verification.
Fiber density, shaft material, adhesive points, and packaging can change sterilization performance. The tested configuration should match the ordered length, tip size, and pouch format. A clean certificate alone is insufficient.
Confirm minimum order quantity, sample policy, production lead time, inspection method, carton size, and delivery terms. Also request analysis certificates and traceability records. Low prices may become costly when replacements arrive late.
Recheck shedding, sizing, residue, packaging integrity, and storage performance. Record defects with lot numbers and photographs. The first shipment may challenge earlier assumptions. That is useful.
This guide presents a practical 2026 framework for global buyers sourcing Ultra-Fine Cotton Swab products. It explains key specifications, including fiber fineness, tip dimensions, shaft materials, packaging options, intended applications, and buyer requirements such as order quantities, customization, documentation, and delivery expectations. The overview also outlines how to evaluate suppliers through ISO 13485:2016 quality management practices and alignment with applicable QMSR requirements.
Additional sections describe manufacturing controls based on ISO 2859-1 AQL sampling, helping buyers assess defects, consistency, and batch acceptance. Sterility validation is addressed through ISO 11135 and ISO 11137 principles, with attention to process qualification, packaging integrity, and traceability. Finally, the guide compares international suppliers using practical criteria such as EU MDR 2017/745 readiness, total cost, production capacity, communication, and lead times, enabling buyers to make informed, compliant, and cost-effective sourcing decisions.
Xiaomianjia Medical